The hidden maintenance trap that turns a used concrete plant into a cash drain
The Plant That Cost More Than a New One
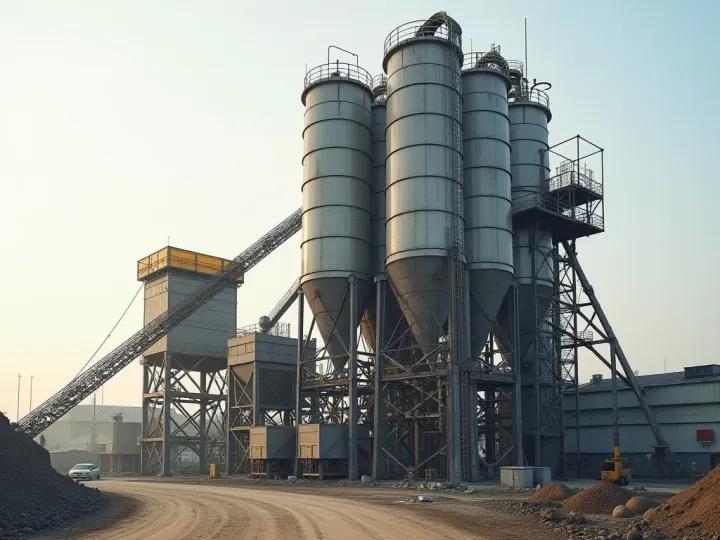
I was sitting in East St. Louis last Tuesday, watching a buyer stare at a listing for a Johnson Ross YD. The price tag said call for quote. That silence is louder than any number on the screen.
Here's the thing about used batching plants. They don't fail all at once. They bleed you slowly through tiny delays, mixed batches that miss spec by two percent, and a mixer seal that keeps weeping hydraulic fluid onto your aggregate bins.
A Con-E-Co SLP sitting in the same yard looks like a bargain. But I've seen three of those units go down within six months of purchase because nobody checked the control system firmware before signing.
Why Old Plants Are Traps in Disguise
Manufacturers design control systems to last roughly ten years before major electronic components degrade. A unit is already past that threshold unless every circuit board was replaced.
So what happens when you buy a machine with aging electronics? You get ghost readings. The scale says , pounds of cement went in the drum, but it was actually ,. Your concrete is weaker than spec and clients will notice within two weeks.
I know a paving contractor who lost a $, street contract because his mix failed compression tests. The plant looked fine from the outside. Inside, one load cell had drifted out of calibration by percent.
The Maintenance Math Nobody Shows You
Let's do the real math. A new -cubic-yard plant runs about $, with installation. A comparable used unit from might cost $,. That sounds like a $, saving.
But maintenance on aging plants runs to percent higher than new units in the first two years. You're looking at an extra $, to $, for seals, bearings, and electronic components that are already tired.
Add in the downtime. A new plant might need four hours of maintenance per month. An older one could need sixteen. That's twelve lost production days a year, which wipes out your savings before you even count the risk of a catastrophic failure.
The Silent Failure Pattern I Keep Seeing
Most buyers look at the mixer and ignore the control system. That's where the real money is hiding. The electronics determine whether your batches are consistent, whether your scales read correctly, and whether you can meet project deadlines.
I've inspected plants where the mixer ran perfectly but the batching sequence was off by three seconds per cycle. Over a month of production, that adds up to nearly two tons of over-mixed concrete you're paying for but not using.
The fix costs $ in parts and an afternoon of labor. But if you don't catch it, your monthly material bill quietly creeps up by to percent without anyone realizing why.
What Actually Matters When You Inspect a Used Plant
Stop looking at the paint job. Start pulling maintenance logs from the last months. If there are gaps, walk away. A well-maintained plant has a paper trail that tells you exactly when seals were replaced and which components got serviced.
Ask for the last three months of batch records. Print them out and look at the variance column. You want to see standard deviations under percent on cement and aggregate weights. Anything higher means your mix quality is inconsistent.
Test the scale calibration yourself with known weights before you buy. Bring a set of calibrated test weights if you can, or at least verify that the system matches up against your own truck scales on site.
The Three Questions That Save You Thousands
Question one: when was the control system last updated? If they can't tell you, assume it's been sitting on -era software that no longer gets security patches or compatibility updates.
Question two: what is the current maintenance schedule? A vague answer like we do it as needed means they're reactive, not proactive. You want a documented preventive maintenance plan with dates and parts lists.
Question three: can I see the last major service invoice? If you can't trace where money went into keeping this plant running, there's a good chance it was patched together rather than properly maintained.
The New Plant Argument That Finally Makes Sense
I used to think buying new was always the smart move. Then I did the math on a fleet of three aging plants versus one modern unit with automated batching and remote monitoring.
The new plant cost percent more upfront but cut maintenance labor by half. It also caught batch errors in real time instead of after a client complained. Over five years, the total cost of ownership was actually lower.
That's not always true though. If you're doing low-volume work and can't justify full-time maintenance staff, a well-maintained used plant from or later might make sense. The key is the age of the electronics.
Where the Used Market Still Wins
Portable plants are a different story. A portable unit with under , hours of operation is often in better shape than a stationary plant from the same year because it doesn't sit idle for months.
Look at hour readings first. A portable with , hours and full maintenance records is often a better buy than one with , hours but no documentation. The machine that gets used consistently tends to get maintained properly.
I've bought two portable units in the last three years and both still run like new because the previous owners treated maintenance as non-negotiable. That's what you're really paying for.
The Bottom Line Nobody Wants to Admit
Used plants aren't bad. Bad sourcing is what's bad. The difference between a good deal and a money pit is usually one hour of inspection done right.
I'd rather spend an extra two days vetting a machine than six months fighting with it. The time you save in the first year pays for itself many times over.
If you're shopping right now, check out the silent failure patterns that quietly drain your budget before you sign anything. And if cost is your main concern, understand the real numbers behind what a local plant charges for premium mixes by reading why concrete plants charge premiums.
The market is full of options right now. There are units in East St. Louis, Fort Dodge, and across the Midwest waiting for someone who knows what they're looking at.
Comments ()